
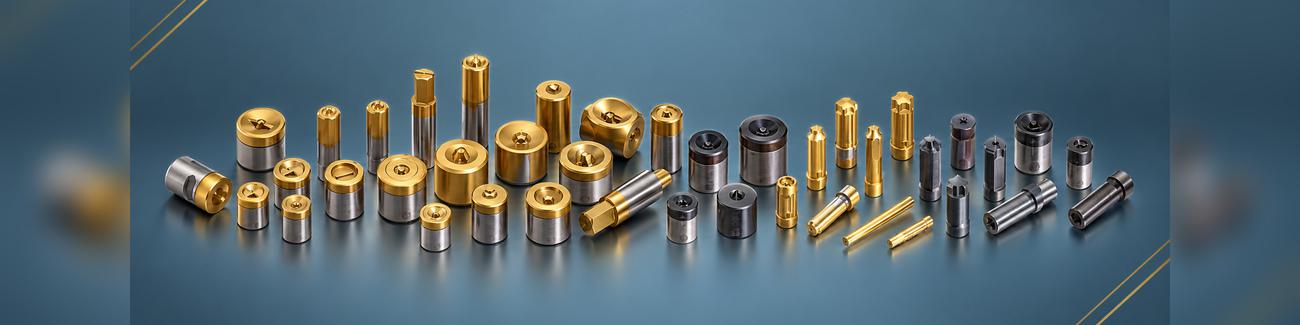
Thread Rolling Dies for Double-End Screws
GXP Click here
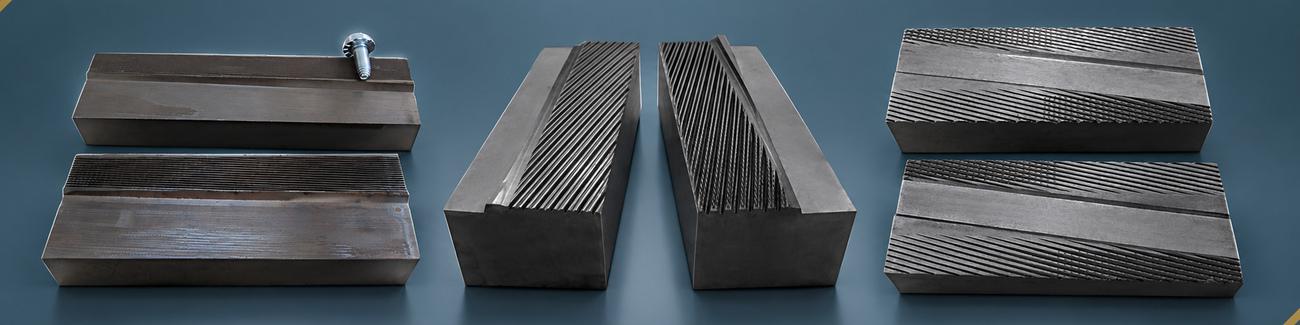
GXP supplies flat thread rolling dies for double-end screw production. Each matched set includes one stationary die and one moving die. Custom specifications can be reviewed according to detailed screw drawings and machine requirements.
Definition and Functions
Double-end screw thread rolling dies are forming tools used to produce external threaded sections at both ends of a screw blank. Pressure between the die plates displaces material into the required thread profile.
Main functions:
- Form the specified thread diameter, pitch and profile at each end.
- Control the length and position of both threaded sections.
- Accommodate a central unthreaded section where specified.
- Match die dimensions to the selected rolling machine.
The website does not confirm whether both ends are rolled simultaneously. The forming sequence and number of die sets depend on the two thread designs, blank geometry and machine capability.
Die Materials
The GXP product page lists the following material options.
| Material | Material Type |
|---|---|
| SKD-11 | Cold-work tool steel for carbon steel used |
| DC-53 | Cold-work tool steel for carbon steel used |
| SKH-9 | High-speed tool steel for stainless steel used |
| M2 | High-speed tool steel for stainless steel used |
Material selection should consider blank material, hardness, thread geometry and production conditions. Confirm the exact grade, heat treatment and any surface treatment during quotation.
Ordering Information
Clearly label both ends as End A and End B on the drawing.
| Item | Required Information |
|---|---|
| Overall dimensions | Total length, blank diameters and dimensional tolerances |
| End A thread | Thread type, diameter, pitch or TPI, direction, tolerance and threaded length |
| End B thread | Thread type, diameter, pitch or TPI, direction, tolerance and threaded length |
| Central section | Unthreaded length, diameter, shoulders or driving features |
| End geometry | Point, chamfer, taper and thread lead-in at each end |
| Blank specifications | Material grade, hardness and dimensions before rolling |
| Machine and dies | Machine manufacturer, model, dimensions of both die plates and mounting details |
| Purchase requirements | Drawing revision, quantity, inspection criteria and requested delivery date |
FAQ
1. What are these dies used for?
They form the specified threaded sections on double-end screw blanks.
2. Can both ends be rolled in one operation?
This requires a feasibility review. Separate operations or die sets may be needed depending on thread geometry and machine capability.
3. Can the two ends have different threads?
Submit each end’s diameter, pitch, profile and threaded length for technical review.
4. Can one end have a right-hand thread and the other a left-hand thread?
Specify the thread direction for each end. The tooling and production sequence must be confirmed before ordering.
5. Which die materials are available?
GXP lists SKD-11, DC-53, SKH-9 and M2. Each matched set contains one stationary die and one moving die.
6. Can the dies preserve a central unthreaded section?
Provide the central section dimensions, tolerances and thread runout requirements for tooling review.
7. What should be checked during trial production?
Inspect each end separately for thread diameter, pitch, direction, profile and length. Also check overall length, central section dimensions, straightness and surface condition.
Request a Quotation
Send GXP your double-end screw drawing with End A and End B specifications, blank details and machine information for technical review and quotation.